Features
Why Choose BELAN?
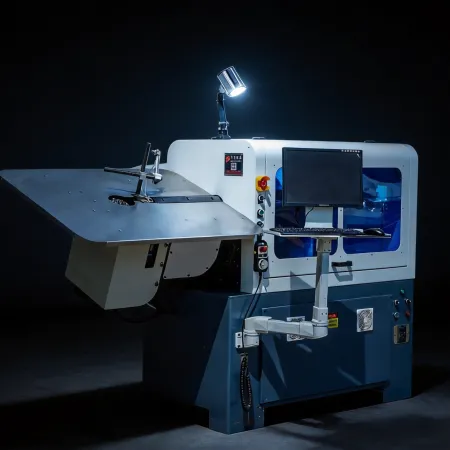
Multi-Axis CNC Precision Control
Advanced multi-axis CNC systems enable precise coordination of feeding, bending, rotating, cutting, and forming processes. This ensures accurate geometry, consistent quality, and stable production performance for complex wire components.
Customized Wire Forming Solutions
Belan provides customized forming solutions based on different wire materials, product structures, and production requirements. From automotive components to special wire parts and busbar applications, we help customers select the right machine configuration for their needs.
High Accuracy & Repeatable Production
Servo-controlled systems and precision mechanical structures deliver excellent feeding accuracy and bending consistency, helping manufacturers maintain stable product quality during continuous production.
Integrated Automatic Forming Process
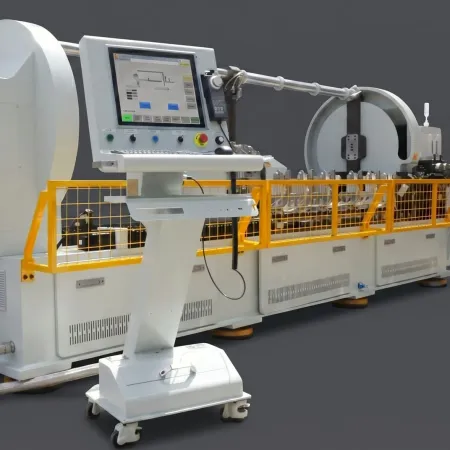
Belan machines integrate multiple processes including wire feeding, straightening, bending, rotating, cutting, and forming into one automated workflow, reducing manual operations and improving overall production efficiency.
We Have The Best Solutions for Your Business
DONGGUAN BELAN AUTOMATION EQUIPMENT CO.,LTD stands at the forefront of the global wire forming industry. Located in the manufacturing heartland of Dongguan, we specialize in high-end 2D and 3D wire forming solutions that merge German precision with Chinese agility.
By integrating advanced CNC technologies from Japan and Korea, we have solved the industry's most persistent challenges: achieving micron-level precision while maintaining high-speed production stability.
Wire Forming Machine: Types, Specifications, and Selection Guide
Introduction
On a production floor, a wire component's cost and quality are rarely decided by one dramatic factor. They are the sum of repeatable details — a bend that holds tolerance on the first and ten-thousandth piece, a setup a new operator can repeat without relearning, a line that keeps its accuracy through a full shift. A wire forming machine takes that logic a step further than a simple bender: it combines bending, rotary forming, torsion, and cut-off into a single automated sequence, so finished parts leave the machine complete rather than moving between stations. Choosing the right one shapes cost, quality, and throughput for years.
This guide explains what a wire forming machine is, how CNC models turn a program into finished parts, the main machine types, the specifications that actually affect production, and how to evaluate a machine against your own components.
What Is a Wire Forming Machine?
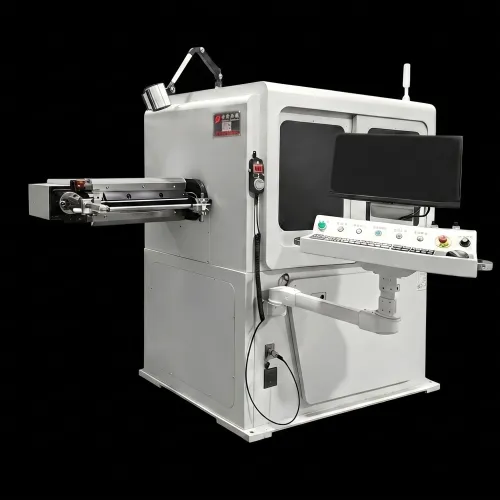
A wire forming machine converts straight or coiled wire into finished shaped components by bending, rotating, and cutting it to a programmed sequence. Where a basic wire bender produces a bend or two and stops, a forming machine carries the part through every operation — feed, rotate, bend, twist, cut — in one uninterrupted setup. The output is a complete component, not a partially processed blank.
In a manual or semi-automatic process, an operator moves the wire between bending fixtures, hand-tools the torsion step, and cuts the finished part separately. In a CNC wire forming machine, the entire sequence is programmed. Servo axes feed, rotate, and form the wire to a stored program, and the finished piece is cut and ejected automatically. The result is less dependence on operator skill and far tighter consistency across a run. For a direct comparison, see our article on automatic wire bending machines versus manual forming.
How Does a CNC Wire Forming Machine Work?
A CNC wire forming machine converts a part program into coordinated servo motion that runs the full forming sequence. The process begins with wire fed from a spool or straightener into the forming head. The feed axis advances a precise length, the wire rotates around its own axis to present the correct plane, and bending or rotary tools form each feature in turn. Torsion and twisting operations are completed within the same sequence, and the finished part is cut and ejected without leaving the machine.
Accuracy depends on two things working together: how precisely the machine holds wire position, and how consistently the tooling forms the material. The controller repeats axis positions to tight tolerances, but the final shape is set where the wire meets the tooling. This is why machine precision and formed-part accuracy are related but not identical, and why tooling, wire support, and setup discipline matter as much as the servo system. For a step-by-step view of the cycle, see our article on how a CNC wire bending machine works.
Most wire materials recover a small amount after a bend is released — a behaviour called springback. CNC machines handle this by calculating the over-bend and holding it in the program, and more advanced systems refine the correction with sensor feedback or AI-assisted compensation that adapts to batch variation. Stable springback handling keeps angles consistent across thousands of parts without an operator re-correcting each one, which is one of the main reasons CNC accuracy outperforms manual setups on long runs.
Types of Wire Forming Machines
Wire forming machines are commonly grouped by the geometry they produce and by how the forming head is arranged.
- 2D wire forming machines — form parts that lie essentially in a single plane, such as brackets, clips, shelves, and simple frames, at high speed in one uninterrupted sequence. See the 2D wire bending machine overview.
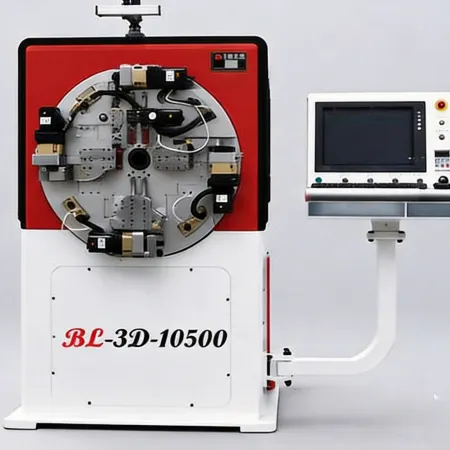
- 3D wire forming machines — add rotation and additional axes so the wire can be bent, twisted, and cut in multiple planes, producing seat frames, complex automotive wire, and three-dimensional forms in a single setup.
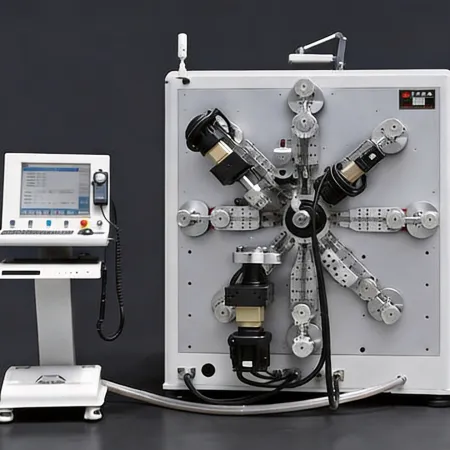
- Rotary head machines — rotate the forming head around the stationary wire, enabling high-speed multi-plane forming with smooth transitions between bends and torsion. See the rotary head CNC wire bending machine.
- Double head machines — form both ends of a part at the same time, which suits symmetrical components and can roughly halve the cycle for the right geometry. See the double head wire bending machine.
The choice is not about which machine is more advanced — it is about matching the architecture to the part. A flat bracket does not need a 3D machine, and a three-dimensional seat frame cannot be made on a 2D one. The article comparing 5-axis and 6-axis CNC wire bending machines explains how axis count changes what a machine can form, and the piece on the advantages of a 3D wire bending machine covers what 3D capability unlocks for complex parts.
Key Specifications That Matter
When evaluating a wire forming machine, a long specification sheet is less useful than a short list of figures that actually predict production performance.
- Wire diameter range — the minimum and maximum wire the machine can feed, rotate, and form reliably, which also sets the forming force requirement.
- Bending and forming accuracy — how closely the machine reproduces angles, radii, and torsion positions part to part, usually expressed as a tolerance band.
- Number of axes — more axes generally mean more operations (bend, twist, cut) can be completed in one setup without manual repositioning.
- Feed and cycle speed — how fast the wire advances and the machine completes a full part, a major driver of throughput.
- Tooling and changeover — how quickly tooling can be swapped and the machine reconfigured between parts.
- Production volume and configuration — whether the machine is built for intermittent batches or continuous mass production.
Among these, wire diameter and forming accuracy tend to govern everything else. They determine the machine frame, the servo size, the tooling design, and ultimately part quality. Specifications should be read as a connected system rather than isolated numbers, and confirmed by trial forming on production wire before commitment.
Wire Diameter and Material Considerations
The wire itself is half of every forming decision. Carbon steel, stainless steel, copper, and aluminum behave differently under the same tooling, and each brings its own challenges.
- Carbon steel wire — comparatively stiff with pronounced springback, so tooling must support it firmly and the working radius must be compensated for recovery.
- Stainless steel wire — tends to work harden during forming, requiring stable, well-distributed contact and consistent force to avoid surface and dimensional issues.
- Copper wire — soft and ductile but marks easily, so tool contact surfaces need particular attention to avoid cosmetic defects.
- Aluminum wire — lighter and lower in strength, and can be marred by tooling configured for harder materials.
Wire diameter matters as much as material. Larger diameters demand greater forming force and stiffer support, and magnify any clearance or alignment error. Fine wire is more sensitive to guiding precision and tool surface finish. Tooling, clearance, and support must be matched to the diameter range actually being run, not to a generic setting. The article on wire forming automation and production efficiency shows how these factors combine to affect real output on the floor.
2D vs 3D Wire Forming
The 2D versus 3D distinction is one of the most common sources of mis-specification. A 2D part lies in a single plane: every bend happens around one axis, and the part is flat. A 3D part spans multiple planes, which means the wire must rotate and the machine must control position in three dimensions as it forms.
For a flat bracket, clip, or shelf hook, a 2D machine is usually the efficient choice — fewer axes, faster cycle, simpler tooling. For a seat frame, a three-dimensional automotive component, or any part where the wire leaves the original plane, a 3D machine is required. Attempting a 3D part on 2D equipment means manual repositioning between operations, which removes the consistency advantage of automation. The guide on choosing a wire forming machine for complex 2D and 3D components walks through how to classify a part before selecting the architecture.
A useful rule: classify the part by the number of planes its bends occupy, not by how complicated it looks. A part with many bends in one plane may still be a 2D job, while a part with few bends across two planes is already a 3D job. Matching the machine to the plane count avoids paying for capability you do not need or lacking capability you do.
Tooling and Changeover
Tooling is where a forming machine earns or loses its consistency. The bending and rotary tools shape the wire on every cycle, so their design, fit, and wear directly determine part accuracy. Custom tooling is often required when a part has a unique radius, an unusual material, or a combination the standard toolset cannot hold.
Changeover is the other half of the equation. A line that runs one part for months values stability; a line that switches SKUs daily values speed of reconfiguration. Quick-change tooling, stored programs, and clear setup documentation reduce the time a machine sits idle between jobs. The article on how CNC wire bending tooling affects forming accuracy and production consistency explains why tooling is treated as an engineered element rather than a commodity, and how wear is managed across a production run.
Applications Across Industries
Wire forming machines serve a broad range of industries because so many products contain shaped metal wire produced in volume. In automotive manufacturing they produce seat frame wire, foam wire, seat support structures, linkage components, and exhaust hanger parts at very high volumes — a demanding application covered in our automotive wire bending machine applications article. In furniture and hardware they form shelf hooks, display racks, and functional brackets. Appliance, enclosure, and medical device makers use them for frames, guards, and precise formed details.
The requirements differ by sector. Automotive production stresses repeatability at volume and tight tolerances because dimensional errors accumulate in downstream assemblies. Furniture and hardware often prioritize fast changeover across many SKUs. Understanding which pressure dominates your work is the first step in specifying the right machine.
How BELAN Approaches Wire Forming Machines
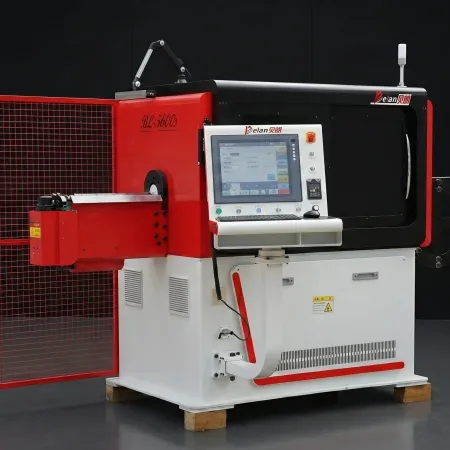
BELAN Machinery builds multi-axis CNC wire bending machines and application-specific forming lines for manufacturers that need repeatable accuracy across demanding wire geometries and materials. Drawing on experience in CNC wire forming, AI-assisted springback compensation, and high-volume automotive wire forming, the engineering workflow starts from the part rather than from a standard machine.
- Review the part drawing and define every bend, radius, torsion, and tolerance
- Confirm the wire specification — material, diameter, and temper
- Select or design tooling around the part geometry, including custom tooling where a unique radius or material requires it
- Configure the machine architecture to match the forming concept
- Trial form with production wire and measure the result
- Lock the proven tooling and parameters for repeatable production
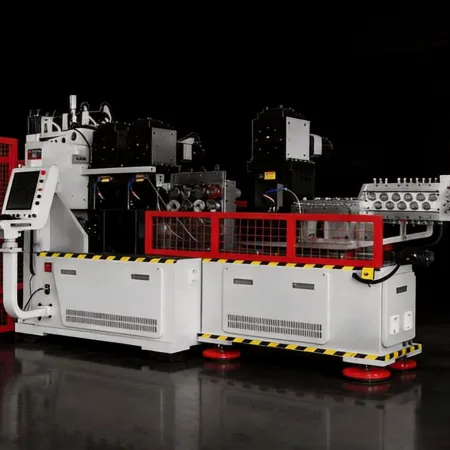
Where a unique bend radius, special material, or complex sequence takes the requirement beyond standard tooling, BELAN designs custom tooling and machine configurations for that specific combination. The decision is driven by the forming requirement, never the reverse, which is also why BELAN's automotive forming lines — such as the automotive seat frame wire forming machine and automotive wiper rod forming machine — are built around the part family rather than a generic platform.
Wire Forming Machine Selection Checklist
- ☐ Define the wire material and diameter range you will actually run
- ☐ List every bend, radius, torsion, and tolerance from the part drawing
- ☐ Decide whether the part is 2D or 3D, and how many planes it spans
- ☐ Estimate production volume and the required cycle time
- ☐ Confirm the accuracy and repeatability your assembly demands
- ☐ Review tooling changeover needs across your SKU mix
- ☐ Check space, power, and upstream handling (spool, straightener)
- ☐ Request trial forming on production wire before commitment
- ☐ Verify after-sales support, training, and spare parts availability
- ☐ Compare total cost of ownership, not just the purchase price
Conclusion
A wire forming machine is only as dependable as the system around it — the program, the tooling, the wire, and the discipline of the setup. The manufacturers who get lasting value are the ones who match machine architecture to the part, validate specifications by forming production wire, and treat tooling as an engineered element rather than a commodity. Done well, the machine stops being a source of variation and becomes a predictable, repeatable foundation for the whole production line.
Whether the requirement is a simple 2D clip or a complex 3D automotive component, the path is the same: start from the part, confirm the material and tolerance, and choose a machine and tooling combination that can hold those specifications across the full production run.
Ready to Evaluate a Wire Forming Machine for Your Parts?
BELAN Machinery, a professional provider of automotive wire forming solutions. Send us your product drawings and wire specifications, including diameter, material, and forming requirements. Our engineering team can evaluate your parts and recommend a suitable machine and tooling configuration.
Contact Belan for a Feasibility AssessmentRelated Resources
- CNC Wire Bending Machines — Overview of BELAN's multi-axis CNC wire bending and forming equipment.
- How to Choose a Wire Forming Machine for Complex 2D and 3D Components — Classify your part and select the right machine architecture.
- Rotary Head Wire Forming Equipment — Multi-plane high-speed forming with smooth transitions between bends.
- Wire Forming Automation and Production Efficiency — How integrated forming affects real throughput on the production floor.
- CE Certified Wire Bending Machines — Why compliance matters for the European market and export projects.
Featured Products
Collection about BELAN
User Reviews
What users say about BELAN
Frequently Asked Question
Do you have any question?
A wire forming machine converts straight or coiled wire into finished shaped components by bending, rotating, and cutting it to a programmed sequence. Unlike a basic bender that produces one or two bends, a forming machine carries the part through every operation — feed, rotate, bend, twist, cut — in a single automated setup, so a complete component leaves the machine rather than a partially processed blank.
Wire bending usually refers to creating bends in wire, often as one or two operations. Wire forming describes the broader process of turning wire into a finished component that may require bending, rotary forming or torsion, and cut-off in one uninterrupted sequence. In practice, a CNC wire forming machine performs both, but the term "forming" signals a more complete, multi-operation part.
Most CNC wire forming machines handle carbon steel, stainless steel, copper, and aluminum across a defined diameter range that varies by model. Larger diameters need greater forming force and stiffer support, while fine wire is more sensitive to guiding precision. The right machine is selected around the material and diameter you actually run, confirmed by trial forming on production wire.
If every bend in your part lies in a single plane, a 2D machine is usually the efficient choice. If the wire must leave that plane and bend in multiple directions, you need a 3D machine. A useful way to decide is to count how many planes the bends occupy, not how complicated the part looks — a few bends across two planes is already a 3D job.
Price depends on axis count, wire diameter capacity, forming force, and whether custom tooling or a dedicated line is required. Beyond the purchase price, the more meaningful figure is total cost of ownership — tooling wear, changeover time, energy, and after-sales support all affect the real per-part cost. Requesting trial forming on your own wire is the reliable way to validate the investment.
Routine maintenance focuses on the parts that touch the wire and repeat every cycle: bending and rotary tools, guides, and feed mechanisms. Scheduled inspection, timely tool replacement, lubrication of moving axes, and operator training keep accuracy stable. BELAN provides after-sales support, training, and spare parts to keep machines running in production.
Our updates and blog posts
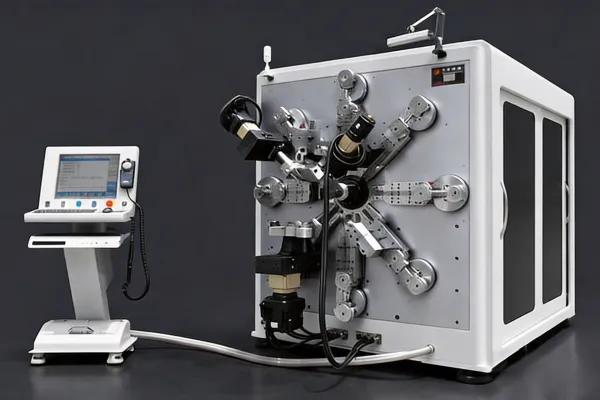
Busbar Bending Machine: CNC Precision Engineering for Modern Power Distribution Manufacturing
Complete guide to CNC busbar bending machines: types, components, materials, bend types, applications, quality standards. Belan TP Series. CE and ISO 9001.
Busbar Bending Machine: CNC Precision Engineering | Belan
CNC busbar bending machine technology: servo-hydraulic systems, closed-loop angle measurement, springback compensation, CAD integration. Belan TP Series.